Table of Contents
Dimensional Challenge & Scaling Objectives
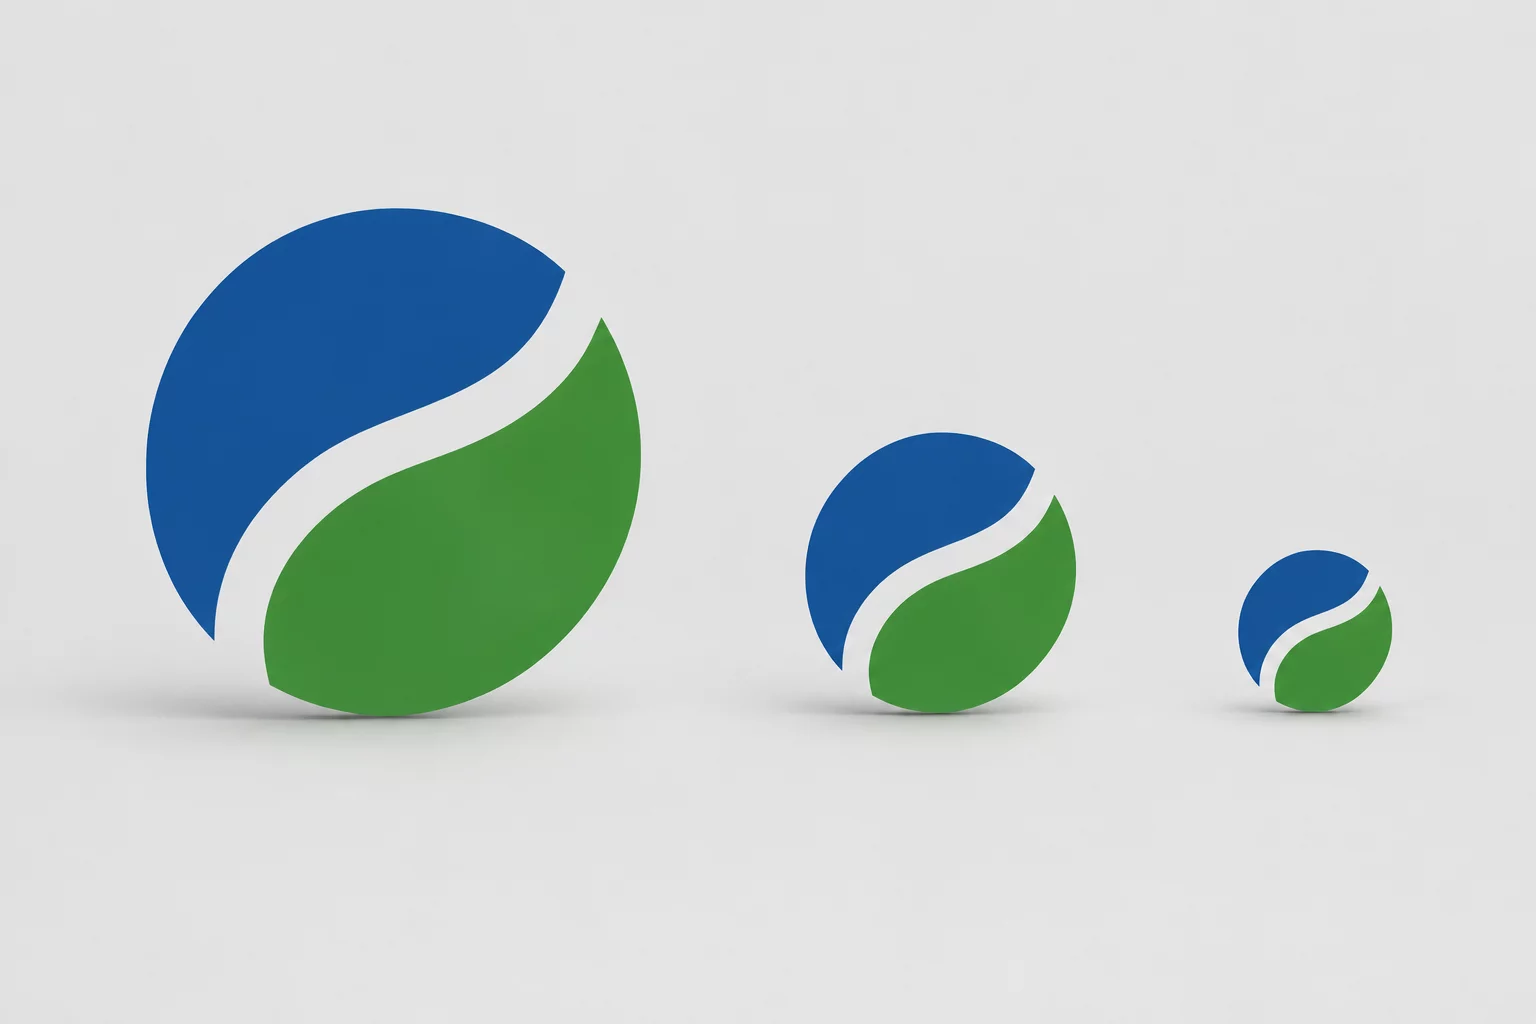
Corporate emblems frequently require reproduction across radically varied media, ranging from storefront fascia signage down to lapel pins, vinyl stationery badges, and compact promotional hardware. When an identity system optimized for billboard and digital screen displays undergoes physical cutter plotting, subtle geometric subtleties become mechanical liabilities. In this case study, we evaluate an emblem originally drafted within an 120 mm envelope and scaled down sequentially to 60 mm, 36 mm, and a terminal micro-scale of 24 mm.
The primary challenge centers on path interference: hairline decorative insets that measure a comfortable 1.5 mm at large scale collapse to a negligible 0.3 mm at 24 mm width. At that density, vinyl adhesive shears, cutting carriage inertia distorts tangent nodes, and weeding tweezers tear fragile structural boundaries. Systematically reviewing each scale tier allows drafters to identify precisely where decorative geometry must yield to physical machine constraints.
Fabrication Tolerances & Thresholds
| Specification Parameter | Verified Tolerance | Standard Threshold |
|---|---|---|
| Minimum Negative Space Gap | 0.85 mm at 24 mm target size | 0.50 mm baseline cutter clearance |
| Outer Contour Stroke Thickness | 1.20 mm reinforced perimeter | 0.75 mm standard vinyl threshold |
| Vector Node Count (Simplified) | 42 contiguous path vertices | 118 original source nodes |
| Tangential Blade Offset | 0.25 mm micro-swivel compensation | 0.30 mm default blade offset |
Scaling a logo for fabrication is not mathematical magnification; it is the art of redistributing mass so the eye perceives the identical mark while the machine blade cuts clean boundaries.
Vector Path Optimization & Blade Clearance
Mechanical plotters navigate paths through sequential coordinates rather than continuous optical sweeps. When vector files simply shrink without node consolidation, clusters of microscopic coordinates force the plotter carriage to stutter, dragging the blade tip through delicate vinyl backings. During our initial benchmark cut at 24 mm, the unedited vector geometry produced three severe tears along acute interior corners.
- Internal counter spaces smaller than 0.6 mm were bridged or excised entirely to prevent adhesive failure during the mechanical weeding phase.
- Acute angles under 25 degrees were softened with micro-fillets to eliminate trailing blade lift and vinyl corner bunching.
- Bézier handles across primary curves were converted into unified arc segments, reducing path complexity by 64% without altering the perceived optical silhouette.
After enforcing these path modifications, the physical sample test yielded crisp separation lines on 651-grade polymeric intermediate film. The resulting decal maintained recognizable corporate brand proportions from standard reading distances while resisting edge lift under continuous fingernail scratch tests.
Final Assessment & Fabrication Rules
Direct proportional scaling consistently breaks physical fabrication workflows once dimensions drop below 40 mm. Corporate brand guidelines must provide three discrete vector master files: one for standard large-format display, an intermediate version with bolstered stroke weights for medium utility, and a consolidated micro-variant where non-essential decorative piercings are eliminated. Applying these parameters ensures consistent legibility, durable vinyl adhesion, and zero production scrap across all production runs.
Download Vector Calibration Guides
Receive technical tolerances, node consolidation benchmarks, and physical cut verification sheets directly to your inbox.
Technical Log Observations
Fieldbook Review ChannelNo comments yet. Be the first to leave a comment.
Submit Observation Note